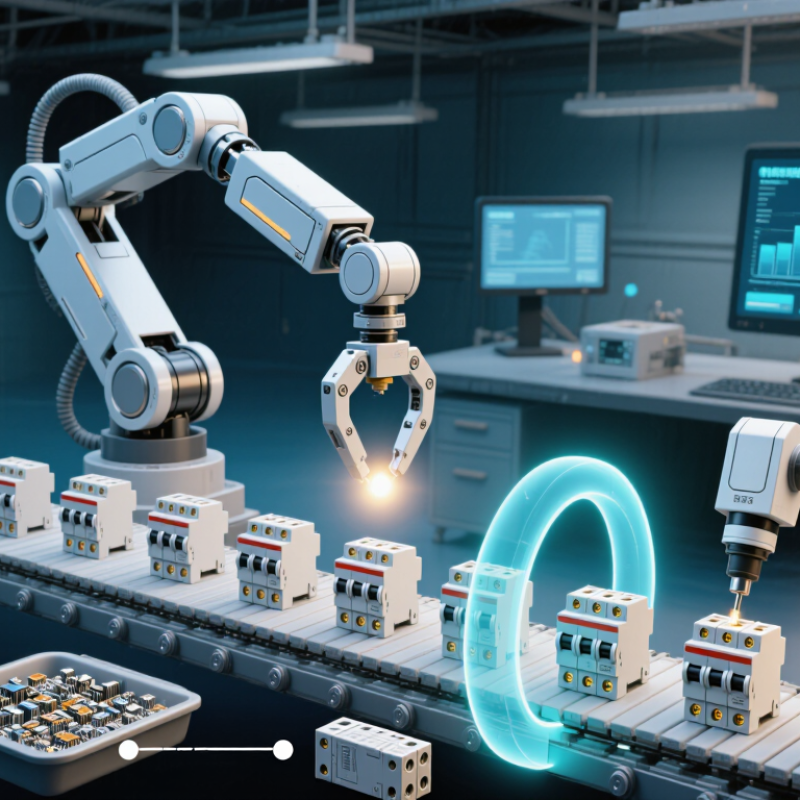
| Component feeding | Hoppers, vibratory feeders, conveyors, and presence sensors | Components such as molded housings, contacts, springs, and operating parts are supplied to the assembly stations in a controlled orientation. | Sensors check that parts are available; vision systems may verify orientation or detect visibly incorrect parts. |
| Part picking and positioning | Pick-and-place robot, gripper, and machine vision | The robot picks selected parts and places them into a fixture or directly into the breaker housing. | Position checks confirm that a part is present and seated before the next operation begins. |
| Internal mechanism assembly | Robotic handling, guided insertion tools, and assembly fixtures | The mechanism and related components are assembled in the arrangement specified by the product design. | Presence, position, and sequence checks help identify missing or incorrectly placed components. |
| Screw fastening or joining | Automatic screwdrivers or other design-appropriate joining equipment | Fasteners or other specified joining features secure the assembly. The method depends on the breaker construction. | For screw fastening, the station can monitor parameters such as torque and angle and flag results outside configured limits. |
| Cover closure and marking | Pressing or closure station, label applicator, and code marking equipment | The housing is closed and required identification or traceability information is applied. | Checks may verify closure, label presence, and whether printed or marked information is readable. |
| Electrical and mechanical testing | Automated test fixtures and measurement instruments | Depending on the product and test plan, completed units may undergo checks such as continuity, dielectric withstand, or operating-mechanism tests. | Results are compared with product-specific acceptance criteria; failed units can be rejected or routed for review. |
| Sorting and traceability | Programmable logic controller (PLC), reject gate, and production data system | The control system coordinates station steps and directs completed products to the appropriate output path. | Production records can associate test results and station status with a batch or product identifier, where traceability is implemented. |

.svg)