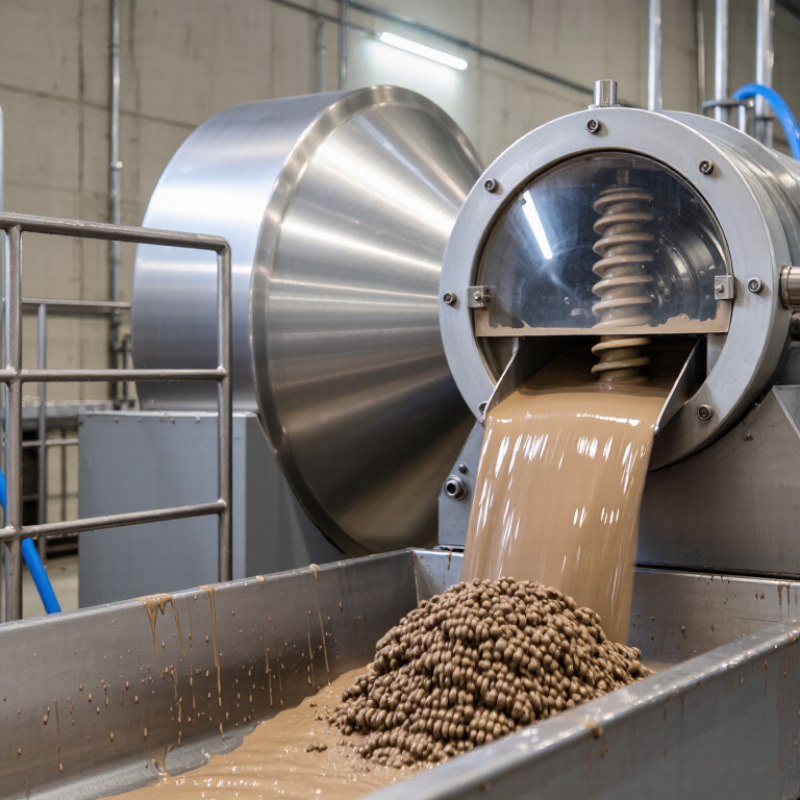
| Why a Screw Centrifuge Is Considered |
| Process suitability | Sludge types | Municipal, industrial, biological, chemical, and mixed sludge | A screw centrifuge can handle continuously fed sludge streams, provided the feed characteristics are evaluated through testing and the equipment is correctly configured. |
| Footprint | Installation area | Generally compact compared with many gravity-based systems | The compact, enclosed layout can be useful where floor space is limited. Allow additional room for polymer preparation, conveyors, maintenance access, and lifting equipment. |
| Operation | Continuous dewatering | Suitable for steady, automated operation | Continuous feeding and automatic torque or differential-speed control can reduce the need for frequent manual intervention, although routine inspection remains necessary. |
| Environmental control | Enclosed construction | Enclosed bowl and conveyor assembly | The enclosed design can help control splashing and odors compared with open dewatering equipment. Ventilation and odor treatment may still be required. |
| Key Factors for Selecting a Screw Centrifuge |
| Feed characteristics | Feed solids concentration | Often about 0.5%–8% total solids | The actual acceptable range depends on sludge type, viscosity, particle size, polymer performance, and machine design. Confirm the range with pilot testing or supplier process data. |
| Feed characteristics | Feed flow rate | Project-specific; commonly measured in m³/h | Select capacity using both hydraulic flow and dry-solids loading. A machine that handles the liquid flow may still be undersized for the required dry-solids throughput. |
| Feed characteristics | Total solids loading | Expressed as kg of dry solids per hour | Use average and peak loading values. Consider seasonal changes, storm flow, process upsets, and future expansion when determining the design capacity. |
| Dewatering target | Cake solids | Often about 15%–30% total solids | The result varies significantly with sludge type, organic content, polymer selection, centrifuge settings, and the required solids capture. The target should be established through testing. |
| Liquid quality | Solids capture | Frequently targeted above 95% with optimized operation | High capture is not automatic. It depends on polymer conditioning, feed stability, bowl speed, differential speed, pond depth, and hydraulic loading. |
| Sludge properties | Particle size and grit content | Must be evaluated before final selection | Abrasion from grit can increase wear on the bowl, conveyor flights, feed zone, and discharge components. Upstream screening or grit removal may be necessary. |
| Material selection | Wetted-part materials | Stainless steel and wear-resistant components are commonly considered | Material selection should reflect chloride concentration, pH, temperature, abrasive solids, and cleaning chemicals. Corrosion and wear requirements should be specified separately. |
| Automation | Control functions | Torque, vibration, speed, flow, and polymer-dose monitoring | Automatic control can stabilize operation and protect the machine, but alarms, interlocks, and control limits must be commissioned for the actual sludge characteristics. |
| Utilities | Power, water, and polymer requirements | Depends on capacity and process configuration | Estimate electrical demand, dilution or flushing water, polymer consumption, compressed air if used, and the availability of drainage and washdown facilities. |
| Important Operating Parameters |
| Centrifuge setting | Bowl speed | Commonly about 1,500–3,500 rpm, depending on equipment size | Higher speed generally increases centrifugal force and may improve clarification, but it can also increase power use, wear, and shear. Adjust within the manufacturer’s permitted range. |
| Centrifuge setting | Differential speed | Often about 1–20 rpm | A lower differential speed usually provides longer solids residence time and may produce drier cake, while a higher speed can increase solids conveying capacity. Monitor torque and centrate clarity. |
| Centrifuge setting | Pond depth | Adjusted according to cake dryness and centrate clarity | A deeper pond can improve liquid clarification but may reduce cake dryness. A shallower pond can increase beach length and drainage, but may affect capture and torque. |
| Feed control | Hydraulic feed rate | Set below the tested maximum for stable operation | Excessive flow can reduce residence time, worsen centrate quality, and overload the conveyor. Increase flow gradually while observing torque, vibration, and liquid quality. |
| Chemical conditioning | Polymer dose | Often approximately 1–10 kg active polymer per tonne of dry solids | The required dose depends on sludge chemistry and polymer type. Use jar testing or pilot trials, and avoid overdosing because it can increase cost and produce sticky cake or poor centrate quality. |
| Chemical conditioning | Polymer maturation | Commonly about 30–60 minutes for many polymer systems | Follow the polymer supplier’s preparation requirements. Incorrect concentration, inadequate aging, or excessive shear can reduce floc strength and dewatering performance. |
| Performance monitoring | Torque | Maintain within the equipment’s normal operating band | A rising torque trend may indicate excessive solids loading, poor polymer conditioning, high differential speed, blocked discharge, or abnormal sludge properties. |
| Performance monitoring | Vibration and bearing temperature | Trend against the machine’s commissioned baseline | Unexpected increases can indicate imbalance, wear, misalignment, bearing problems, or foreign material. Investigate abnormal trends before continuing at full load. |
| Operating and Maintenance Practices |
| Start-up | Pre-start inspection | Before every operating shift or automatic start | Check guards, lubrication status, polymer availability, feed and discharge paths, wash-water supply, emergency stops, vibration alarms, and equipment cleanliness. |
| Start-up | Clean-water or low-load start | Use the equipment’s approved start-up sequence | Allow the bowl to reach operating speed before introducing sludge, then introduce feed gradually. This reduces the risk of sudden torque spikes and unstable separation. |
| Normal operation | Parameter adjustment | Change one major variable at a time | Make small, controlled adjustments to feed rate, polymer dose, differential speed, or pond depth. Allow sufficient stabilization time before judging the result. |
| Shutdown | Flushing and cleaning | After each operating cycle or as required by sludge type | Flush residual solids from the feed zone, bowl, conveyor, and discharge areas according to the operating manual. Proper cleaning helps prevent hard deposits and imbalance. |
| Maintenance | Wear-part inspection | Based on hours, grit loading, vibration, and observed wear | Inspect conveyor flights, wear tiles, feed components, discharge nozzles, seals, bearings, and lubrication systems. Abrasive sludge may require shorter inspection intervals. |
| Safety | Lockout and guarding | Required before maintenance or entry into hazardous areas | Isolate electrical and mechanical energy, verify zero energy, and prevent access to rotating equipment. Only trained personnel should operate or service the centrifuge. |
| How to Compare a Screw Centrifuge with Other Dewatering Options |
| Compared with belt filter presses | Space and enclosure | Usually more compact and more enclosed | A screw centrifuge may be preferred where footprint and odor containment are important. A belt press may offer simpler visual inspection and lower rotational speed. |
| Compared with filter presses | Process mode | Continuous rather than batch operation | A screw centrifuge supports continuous throughput, while a filter press can produce higher cake solids for some sludges but requires batch cycles and cloth maintenance. |
| Compared with screw presses | Separation mechanism | Centrifugal separation with a rotating bowl | A centrifuge can provide strong clarification and compact installation, but it may require more electrical power and closer monitoring of vibration, torque, and wear. |
| Lifecycle evaluation | Total cost of ownership | Capital, power, polymer, water, labor, maintenance, and disposal | Do not select equipment based only on purchase price. Compare energy consumption, polymer demand, expected cake solids, centrate treatment, wear-part life, service requirements, and operator workload. |

.svg)