Food Safety Insights

In Eagle’s Advanced Insights Blog, experts share their know-how by keeping you up-to-date with the latest trends to ensure your inspection equipment keeps your products safe. Eagle is an industry leader when it comes to performance and innovation, and we’ll share the news that’s important to you to enhance your quality assurance program.

Suggest topic you would like to see at:

sale@generalmachinery.org

10 Best Food Inspection Machines for Global Buyers

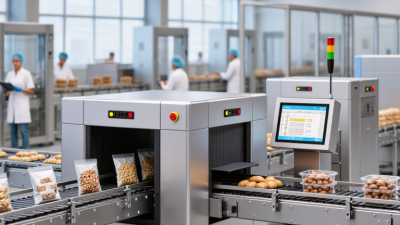
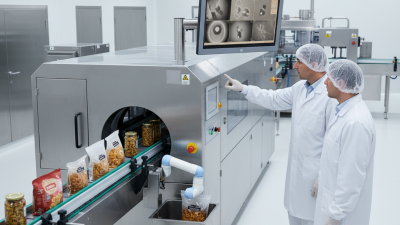
Choosing the right food inspection machine is not a simple equipment decision. It affects product safety, production speed, waste levels, and buyer confidence. A reliable system must detect risks without damaging packaged goods or slowing the line. Metal fragments, glass pieces, dense plastic, incorrect weights, missing products, and damaged seals require different inspection methods.

Food safety expert Dr. Martin Wiedmann puts the responsibility plainly: “Food safety is not a test at the end; it is a system built into every step.” This principle matters for global buyers comparing X-ray inspection, metal detection, checkweighing, vision inspection, and combination systems. Each technology has strengths. None solves every production problem.

Look closely at real operating conditions. A chilled meat line may face condensation, oily surfaces, and rapid belt movement. A bakery may need accurate weight checks beside crowded packaging. A ready-meal producer may prioritize seal inspection and foreign-object detection. Cleaning routines matter, too. So do software records, reject confirmation, calibration access, and operator training.

The best choice is rarely the most expensive model. It is the machine that matches the product, line speed, package material, hygiene design, and local service support. This guide compares ten leading options for global buyers, using practical criteria rather than impressive specifications alone. Some rankings remain debatable. That is worth admitting. Real performance can change after installation, especially when factory conditions differ from supplier demonstrations. Reliable decisions require testing representative products before purchase.

10 Best Food Inspection Machines for Global Buyers

What Food Inspection Machines Are and Why They Matter

Food inspection machines are automated systems that check products for safety, quality, and consistency.

They examine items without stopping every package for manual inspection. Common equipment includes:

Metal detectors
A metal detector can identify ferrous and non-ferrous fragments inside packaged food.
X-ray systems
X-ray equipment may reveal dense foreign material, missing components, or broken products.
Vision cameras
Vision systems inspect labels, colors, shapes, and visible defects.
Checkweighers
Checkweighers compare each package with its target weight.

Their value is practical on a busy production line.

A damaged seal can allow moisture to enter during storage. An incorrect weight can create customer complaints and costly recalls.

Automatic rejection devices remove questionable products within seconds.

Records also show when an event occurred, which line was involved, and how operators responded. These records support traceability, process reviews, and quality audits.

For global buyers, data export, language settings, electrical compatibility, and local service access deserve careful attention.

Yet machines do not replace judgment.

A sensor can miss defects when products overlap or packaging changes. Poor alignment may cause false rejects. No machine is perfect.

Buyers should request tests using real products, including wet, frozen, irregular, and reflective packages.

Ask for rejection samples and verify that alarms are easy to understand. Check cleaning access, calibration procedures, spare parts, and operator training.

It is easy to focus on detection speed and overlook maintenance. A reliable system must fit the product, line speed, hygiene routine, and daily skills of the production team.

Key Technologies Used in Modern Food Inspection

10 Best Food Inspection Machines for Global Buyers

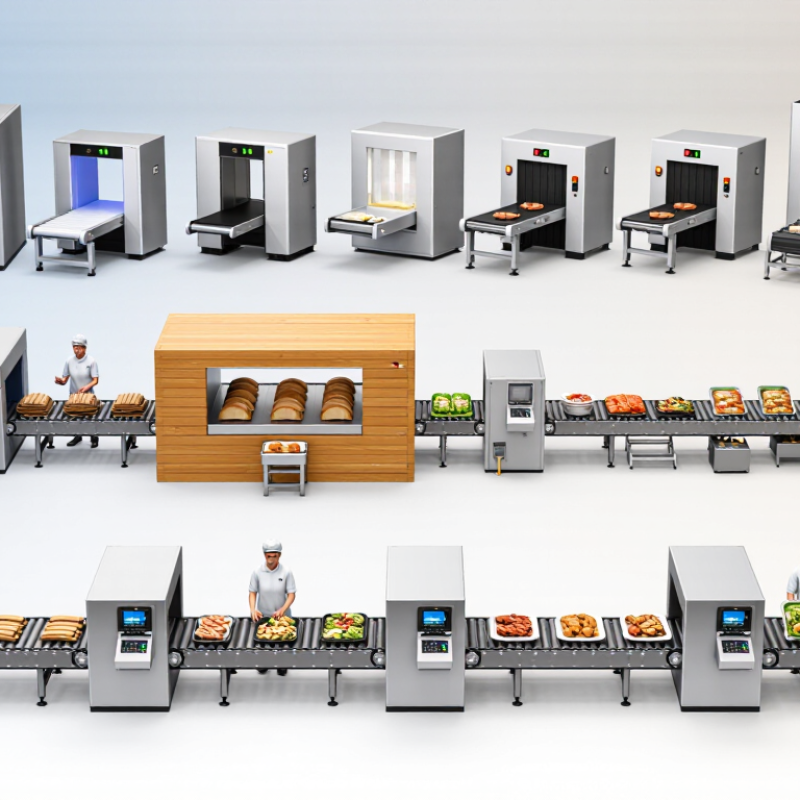
Modern food inspection depends on several technologies working together. X-ray systems detect dense foreign materials, including small metal, glass, or bone fragments. Metal detectors use electromagnetic signals to identify conductive contaminants inside sealed products. Vision inspection checks labels, seals, color, shape, and surface defects at high line speeds. Checkweighers identify underfilled or overfilled packages before shipment.

Hyperspectral imaging can reveal moisture changes, bruising, or unusual ingredients that ordinary cameras may miss. Optical sorters separate products by color, size, and visible quality differences. In practice, detection accuracy depends on product temperature, packaging material, line speed, and calibration. No machine performs perfectly. Trials with real products matter more than impressive specifications.

Tips: Request sample testing before purchase. Measure sensitivity using your actual package sizes. Check data records, cleaning access, and operator training. Confirm that software supports traceability and local inspection requirements. A practical mistake is choosing maximum speed first. Stable detection and simple maintenance often create better results. Consider false rejects, too. Excessive rejection can waste safe food and hide process problems.

10 Best Food Inspection Machines for Global Buyers

Key technologies used in modern food inspection, ranked by the number of primary inspection targets typically addressed.

The comparison covers major inspection technologies used across food processing lines. Higher values indicate a broader range of primary targets, while actual performance depends on product composition, packaging, line speed, and system configuration.

How to Compare the 10 Best Food Inspection Machines

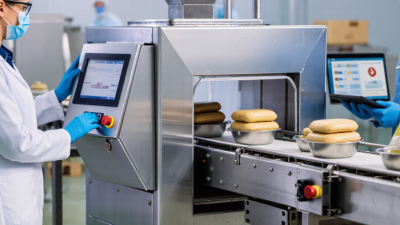
Comparing the 10 best food inspection machines requires more than reading detection claims. Each machine should be tested with the actual product, packaging, speed, and temperature. A metal detector may suit dry snacks, while an X-ray system can identify dense contaminants and missing components. Vision equipment checks color, shape, labels, and surface defects. Checkweighers verify portion accuracy during continuous production.

Start with detection performance. Ask suppliers for test results using realistic samples, not ideal laboratory pieces. Measure false rejects, conveyor speed, product spacing, and changeover time. Small details matter. A machine that rejects one good pack in every fifty can create serious waste. Review sensor stability, lighting control, belt design, and cleaning access. Stainless construction and suitable protection ratings are important in wet processing areas.

Then compare integration and long-term support. Confirm whether the system connects with existing conveyors, control software, traceability records, and automatic reject devices. Operators should understand alarms without guessing. Training quality often affects reliability more than impressive specifications. Request calibration procedures, maintenance intervals, spare-part availability, and response times. A low purchase price may hide expensive downtime. My practical concern is simple: comparison tables can look precise, but factory conditions rarely stay perfect. Dust, vibration, product variation, and rushed changeovers can weaken performance. Run a supervised trial across several production shifts before choosing a final model.

10 Best Food Inspection Machines for Global Buyers - How to Compare the 10 Best Food Inspection Machines

No. Machine Type Primary Inspection Purpose Typical Contaminants or Defects Detected Typical Throughput Suitable Product Formats Main Detection Technology Key Buying Considerations
1 Conveyor Metal Detector Continuous detection of metallic contamination in unpackaged or packaged food. Ferrous, non-ferrous, and stainless-steel particles. Up to approximately 120 m/min Bags, boxes, trays, bakery products, meat, and produce Electromagnetic field analysis Aperture size, product effect, sensitivity, washdown rating, and reject mechanism.
2 Food X-Ray Inspection System Inspection of packaged food for dense foreign objects and selected quality faults. Glass, stone, mineral bone, metal, calcified bone, and some high-density plastics. Approximately 30–100 m/min Cans, cartons, pouches, jars, bottles, and multipacks Low-energy X-ray imaging Product density, package dimensions, radiation-safety compliance, image resolution, and software functions.
3 Dynamic Checkweigher Verification of product weight and removal of underweight or overweight packs. Missing components, underfill, overfill, and incorrect portion weight. Up to approximately 400 packs/min Pouches, cartons, trays, jars, bottles, and flow-wrapped packs Load-cell weighing while products are moving Weighing range, accuracy, line speed, legal-for-trade requirements, and data connectivity.
4 Vision Inspection System Automated visual inspection of appearance, position, labeling, and package integrity. Wrong labels, missing components, color variation, shape defects, dents, and damaged packaging. Approximately 60–600 products/min Bottles, cans, cartons, trays, jars, and individual products Industrial cameras, controlled lighting, and image-processing software Camera resolution, lighting design, inspection coverage, recipe management, and false-reject rate.
5 Seal and Package Integrity Tester Detection of leaks and weak seals that could reduce shelf life or cause contamination. Channel leaks, incomplete seals, weak heat seals, pinholes, and damaged closures. Approximately 20–300 packs/min Flexible pouches, vacuum packs, trays, cans, bottles, and sachets Pressure decay, vacuum decay, force measurement, or non-destructive leak testing Test sensitivity, destructive or non-destructive operation, package material, and test-cycle time.
6 Optical Sorter Sorting of bulk food products by color, size, shape, and visible quality characteristics. Discoloration, mold-related visual defects, stones, stems, shells, and foreign material with optical contrast. Approximately 2–15 tonnes/hour Grains, nuts, pulses, seeds, fruit, vegetables, and frozen products RGB, monochrome, infrared, or multispectral cameras with air-jet ejection Feed consistency, channel capacity, color range, compressed-air consumption, and sorting accuracy.
7 Hyperspectral Imaging System Advanced inspection of composition, freshness, moisture distribution, and hidden quality variation. Early spoilage indicators, foreign material, bruising, moisture variation, and compositional differences. Approximately 10–80 m/min Meat, seafood, fruit, vegetables, grains, and powders Visible and near-infrared spectral imaging Model calibration, spectral range, lighting stability, data-processing capability, and application validation.
8 Fill-Level and Volume Inspection Machine Verification that containers have the correct fill level, volume, and product presence. Underfill, overfill, missing product, foam variation, and incorrect liquid level. Up to approximately 600 containers/min Bottles, cans, jars, cups, and liquid-filled pouches Vision, laser, radio-frequency, or X-ray measurement Container material, liquid opacity, foam behavior, measurement tolerance, and line synchronization.
9 Label and Code Verification System Verification of printed information, barcode readability, and product-to-label matching. Wrong labels, unreadable barcodes, missing date codes, incorrect lot numbers, and print defects. Approximately 100–1,000 packs/min Cartons, bottles, cans, pouches, trays, and cases OCR, OCV, barcode reading, and machine vision Code type, print contrast, database integration, line speed, traceability, and changeover time.
10 Combination Inspection System Integrated inspection of contamination, weight, package condition, and product identity on one line. Metal, dense foreign objects, underweight packs, damaged packaging, wrong labels, and missing products. Approximately 60–400 packs/min Retail packs, ready meals, meat, seafood, bakery products, and multipacks Combined metal detection, X-ray, checkweighing, and vision inspection Available floor space, integration complexity, total cost of ownership, hygienic design, and service support.

Note: Throughput figures are typical application ranges and vary according to product size, package type, inspection sensitivity, line layout, and machine configuration.

Top Food Inspection Machines for Different Product Categories

Top Food Inspection Machines for Different Product Categories

Food inspection machines should match the product, package, and defect risk.

WHO estimates that 600 million people suffer foodborne illness annually. Around 420,000 people die from it. These figures strengthen the case for layered inspection, not one machine alone.

For canned foods, frozen meals, and dense packaged products, X-ray systems can detect metal, glass, stones, and missing components.

Metal detectors suit bakery items, snacks, and meat products, but moisture can reduce sensitivity.

Checkweighers verify fill accuracy on sealed cartons and pouches.

Vision systems inspect labels, seals, shape, and color.

Optical sorters work well with grains, nuts, vegetables, and fruit.

Leak detectors are useful for vacuum packs and modified-atmosphere packaging.

FAO reports that 13.2% of food is lost before retail, so accurate sorting and weight control also protect usable production.

Still, machine settings are not universal. A system calibrated for dry cereal may perform poorly on wet cheese.

Tips:

Test samples from each product category before purchase.

Include real defects, not perfect laboratory pieces.

Review detection limits, false rejects, cleaning time, and data traceability.

Ask for validation records based on recognized food-safety procedures.

Operators should inspect rejected products regularly.

A low reject rate sounds efficient, but it may hide weak sensitivity.

Human review remains necessary.

Global Buying Factors: Standards, Costs, Service, and Integration

Global buyers evaluate food inspection machines beyond detection accuracy. The right choice must fit product, packaging, throughput, and local compliance requirements. Ask suppliers for documented test procedures, calibration records, and validation data using samples that resemble your products. A machine detecting metal in dry snacks may perform differently with wet, salty, or frozen foods. Recognized standards matter because audit evidence must be clear, repeatable, and easy for operators to understand. Confirm electrical compatibility, hygienic design, protective materials, and data security expectations before purchase. Small details matter.

Cost analysis should include installation, training, spare parts, software updates, energy use, and rejected-product handling. A cheaper quotation can become expensive when belts, sensors, or service visits require long international shipping. Request a realistic response time and written maintenance scope. Remote support helps, but it cannot replace a technician who understands the production line. Integration also deserves a live trial. Check whether inspection results connect with existing conveyors, alarms, traceability systems, and production records. Ask for data formats and failure behavior during network loss. Some projects overestimate automation and underestimate operator training. That is an uncomfortable lesson. Leave space for manual checks, recipe changes, and future product sizes. A practical factory test often reveals more than a polished sales presentation.

Any Questions? We Are Here for You

Contact Us

Contact Us

Request information

Ask us a question
Service Support

Service Support

Available 24 hours a day, 7 days a week.

Get in Touch
Find a representative

Find a representative

Contact your local representative

View Locations