Food Safety Insights

In Eagle’s Advanced Insights Blog, experts share their know-how by keeping you up-to-date with the latest trends to ensure your inspection equipment keeps your products safe. Eagle is an industry leader when it comes to performance and innovation, and we’ll share the news that’s important to you to enhance your quality assurance program.

Suggest topic you would like to see at:

sale@generalmachinery.org

How to Choose a Food X Ray Machine for Your Business?

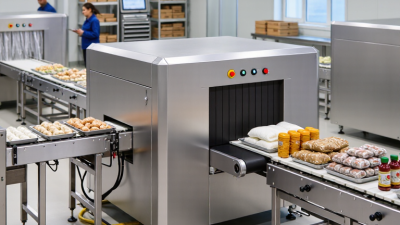
Choosing a food x ray machine is not simply a matter of comparing prices or selecting the fastest conveyor. It means matching inspection performance to your products, packaging, line speed, and daily production realities. A machine that handles dense glass jars may not suit lightweight snack bags. Small details matter: product orientation, belt width, washdown needs, and how quickly operators can review a reject.

Food inspection engineer Alex Morgan captures the decision in this practical reminder: “Choose for the product you actually run, not the one in the brochure.” That principle is useful, though no single quotation can replace a documented site assessment. Buyers should ask suppliers to test representative products, including difficult pack sizes and varied product positions. They should also request clear information about detection capability, routine verification, operator training, maintenance, and service response. Ask to see the test conditions. They matter.

A food x ray machine can help identify physical contaminants and support quality control, but it is not a guarantee of product safety. Performance depends on the product, contaminant properties, packaging, and system setup. There are trade-offs. Higher sensitivity may affect false rejects, while a compact layout can make access harder. It is worth challenging assumptions, including your own. Compare real trial results, not just headline specifications, before choosing equipment for your business.

How to Choose a Food X Ray Machine for Your Business?

Define Your Food Inspection Requirements

Before comparing machines, define what your production line must inspect. List the product types, package materials, and likely foreign-body risks. A sealed pouch, glass jar, and frozen meal present different inspection challenges. X-ray systems detect differences in density, but product thickness and texture can affect results. Small details matter.

Record your usual and largest package dimensions, line speed, and operating conditions. Include product temperature, moisture, and how consistently items sit on the belt. Then decide what detection performance you need and how it will be checked. Test with suitable reference pieces in real products, not only empty packages. Ask how the system handles rejected items, stores inspection records, and alerts operators to faults. A polished specification sheet can feel reassuring, but it cannot prove performance on your line. Trials may expose awkward gaps, such as overlapping packs or unstable products. That is useful information. Be ready to revise your assumptions.

How to Choose a Food X-Ray Machine for Your Business? — Define Your Food Inspection Requirements

Requirement Example Business Need What to Specify Selection and Validation Notes
Product type Packaged snack bars, frozen meals, or bottled sauces Product composition, density variation, temperature, and whether products are solid, liquid, or mixed Request trials using representative products. Product density and shape can affect inspection performance.
Contaminants of concern Metal fragments, mineral stone, glass, or dense bone Target material, approximate size, shape, and likely location in the product Detection depends on contaminant material, orientation, product, and inspection setup. Agree on test pieces and acceptance criteria before purchase.
Package format Pouches, trays, cartons, cans, or glass containers Package material, dimensions, orientation, closure, and product presentation X-ray inspection can be used with many package materials, but the complete package and product should be tested together.
Product dimensions Small sachets alongside large family-size packs Minimum and maximum product width, height, length, and weight Check the usable inspection opening and conveyor width. Allow clearance for product variation and line guides.
Line speed and volume Continuous production with occasional product changeovers Products per minute, conveyor speed, operating hours, and peak production rate Confirm inspection and rejection performance at the actual line speed, including closely spaced products.
Inspection location After sealing, before case packing, or at the end of the line Available floor space, conveyor height, product flow, and access for operators Plan for infeed and discharge conveyors, reject handling, guarding, and safe access for cleaning and maintenance.
Reject handling Remove a single suspect pack without stopping the full line Product spacing, pack stability, reject-bin capacity, and preferred reject method Choose a suitable reject device, such as a pusher, air blast, or drop-down belt, and verify removal without disturbing adjacent products.
Inspection objectives Contaminant detection plus checks for missing or broken items Required checks, product recipes, alarm conditions, and recordkeeping needs Confirm which inspection functions are available for the chosen product and configuration; not every system supports every check.
Washdown and hygiene Wet processing area with routine foam cleaning Cleaning chemicals, water exposure, cleaning frequency, and hygiene procedures Specify the actual cleaning conditions and verify that the equipment enclosure and conveyor design are suitable for them.
Integration and records Connection to a production line and routine quality checks Line signals, data export, user access, product setup, and test-record requirements Define the required interfaces and documentation with the equipment supplier and your quality team before installation.
Acceptance testing Document that the system meets agreed production requirements Test products, test-piece materials and sizes, line speed, test frequency, and pass/fail rules Use a documented protocol under real operating conditions. Set criteria based on risk assessment and applicable food-safety procedures.

Note: Example requirements are for planning purposes. Confirm performance with representative products, packaging, line conditions, and documented acceptance tests.

Match the Machine to Your Products and Production Line

Match the machine to the product first, then the production line. A compact unit may suit small packs, while large frozen blocks need a wider opening and sufficient belt capacity. Product density, moisture, packaging, and orientation all affect image quality. A wet, uneven product can be harder to inspect consistently. Test real samples, not just ideal examples.

Line speed matters. Check the machine’s usable inspection width, belt height, and reject timing against your actual conveyor—not the line’s advertised maximum speed. A glass jar, foil pouch, and loose snack bag present different inspection conditions. Also confirm that rejected products can be removed safely without stopping production.

FAO’s 2019 State of Food and Agriculture estimated that about 14% of food is lost between post-harvest and retail. That figure is not a promise that inspection prevents losses, but it underlines why dependable checks and low false-reject rates matter.

Tips: Run trials with your own products at normal line speed. Record detection results, false rejects, and changeover time. Ask operators to review the reject area, cleaning access, and alarm signals. Small details count. A specification sheet can look perfect; real production may disagree. Recheck after recipe or packaging changes.

Compare Detection Performance and Operating Specifications

A food X-ray machine should be compared using your actual products, not only a stated detection limit. Product density, package material, orientation, and line speed can all affect image quality. Ask for test results using representative samples, including products near the smallest size you need to detect. A result from a dry, uniform sample may not reflect a dense, mixed product. Run real samples.

Compare detection sensitivity with false-reject rates. A system that flags many acceptable products can slow production and increase manual checks. Review how settings are adjusted for different recipes and package sizes, and whether operators can understand alerts quickly. Ask how the machine performs when a contaminant sits near an edge or overlaps a dense ingredient. Small details matter.

Operating specifications deserve the same attention. Check belt width, maximum product dimensions, conveyor speed, power needs, and the conditions the unit can handle, such as washdown or temperature changes. Confirm that reject timing matches your line speed and that rejected items are easy to identify. Request a trial at realistic throughput. It may expose awkward gaps in the process, and that is useful. Compare maintenance access, cleaning time, and image records too; a strong detection result is less valuable if routine operation is difficult.

Verify Safety Standards, Compliance, and After-Sales Support

A food X-ray machine should be assessed against the safety requirements that apply to your market and production line. Ask the supplier to identify relevant standards and provide current certificates, test reports, and operating documentation. Check that the paperwork matches the exact machine configuration, not just a similar model. Small differences matter.

Compliance also depends on how the system performs in your facility. Request a site assessment and test the machine with representative products, packaging, and line speeds. Review reject-device checks, radiation-safety procedures, calibration records, and staff training materials. A neat demonstration is useful, but real production conditions can be less predictable. I would not treat one successful test as proof of long-term performance.

After-sales support deserves the same scrutiny as detection capability. Confirm response times, technician availability, spare-parts access, warranty coverage, and preventive-maintenance options in writing. Ask how faults are diagnosed and what happens if the line stops during a busy shift. Speak with a current customer if possible. A checklist can look complete; I might still miss a practical detail, such as whether service visits can fit your operating schedule.

Evaluate Total Ownership Costs and Validate Supplier Claims

A food X-ray machine’s purchase price is only the visible part of its cost. Build a five-year estimate that includes installation, operator training, electricity, routine calibration, software fees, and scheduled service. Add likely costs for replacement parts and production downtime. Small costs add up. Ask who pays for shipping and labor when a technician visits, and how quickly support is available during a line stoppage. These details can change the economics more than a modest difference in the quoted price. I would also compare the machine’s footprint and cleaning requirements with the space and sanitation routines on your actual production floor.

Treat performance claims as questions to verify, not promises to accept. Ask the supplier to test representative products using your packaging, line speed, and operating conditions. Record what the trial detects, what it misses, and how settings affect false rejects. A polished demonstration is not enough. Request written results, the test setup, and clear acceptance criteria before purchase. If possible, have your own quality staff observe the trial and repeat key checks. One limitation is easy to overlook: results from a sample run may not reflect every product variation or shift. Keep that uncertainty visible in your evaluation, and confirm what ongoing support and performance checks are included.

How to Choose a Food X-Ray Machine: Evaluate Total Ownership Costs

Illustrative five-year cost breakdown for comparing supplier quotations (USD).

This example totals $54,500 over five years, including purchase, installation, training, maintenance, verification, and energy. These figures are planning assumptions, not market benchmarks or supplier quotes. Request itemized costs and validate service coverage, warranty terms, and performance claims before comparing offers.

Any Questions? We Are Here for You

Contact Us

Contact Us

Request information

Ask us a question
Service Support

Service Support

Available 24 hours a day, 7 days a week.

Get in Touch
Find a representative

Find a representative

Contact your local representative

View Locations